
Coal chemical processes involve some of the most demanding pumping conditions in the process industry. High temperature, high pressure, high solids content, severe abrasion and corrosive media place strict requirements on pump reliability, materials, sealing and hydraulic design.
Coal Chemical Centrifugal Pumps are widely used in coal gasification, direct coal liquefaction, coal-to-methanol and coal-to-liquid hydrogenation processes. Typical applications include coal slurry pumps, quench water pumps, lock-hopper circulation pumps, slurry transfer pumps, lean methanol pumps, hydrogenation circulation pumps and hydrogenation feed pumps.

1. Centrifugal Pumps in Coal Chemical Processes
Coal Gasification
Coal gasification systems use pumps for coal slurry transfer, quench water circulation and slag-water handling. Low-pressure coal slurry pumps transport high-concentration slurry from grinding systems to storage tanks, while high-pressure coal slurry pumps deliver slurry to the gasifier.
Quench water, black water and lock-hopper circulation pumps handle high-temperature water containing ash and solid particles. These applications require wear-resistant hydraulic components, reliable mechanical seals and robust pressure-bearing structures.
Direct Coal Liquefaction
Direct coal liquefaction combines high temperature, high pressure and hydrogenation. Hydrogenation circulation pumps and slurry pumps may handle multiphase media containing gas, liquid and solid particles.
For severe high-temperature slurry services, double-casing construction, high-hardness alloys, specialized sealing systems and thermal management are important design considerations.
Coal-to-Methanol
In low-temperature methanol washing systems, lean methanol pumps circulate methanol over a wide temperature range. Horizontal multistage centrifugal pumps with balanced hydraulic design are commonly used where stable operation and reliable sealing are required.
Coal-to-Liquid Hydrogenation
Hydrogenation feed pumps deliver high-temperature and high-pressure oil-based media to reactors. These pumps commonly require high-pressure multistage configurations, double-casing construction and API 610-compliant design for applicable petrochemical services. API 610 defines requirements for centrifugal pumps used in petroleum, petrochemical and natural-gas process services.
2. Key Design Requirements
Double-Casing Construction
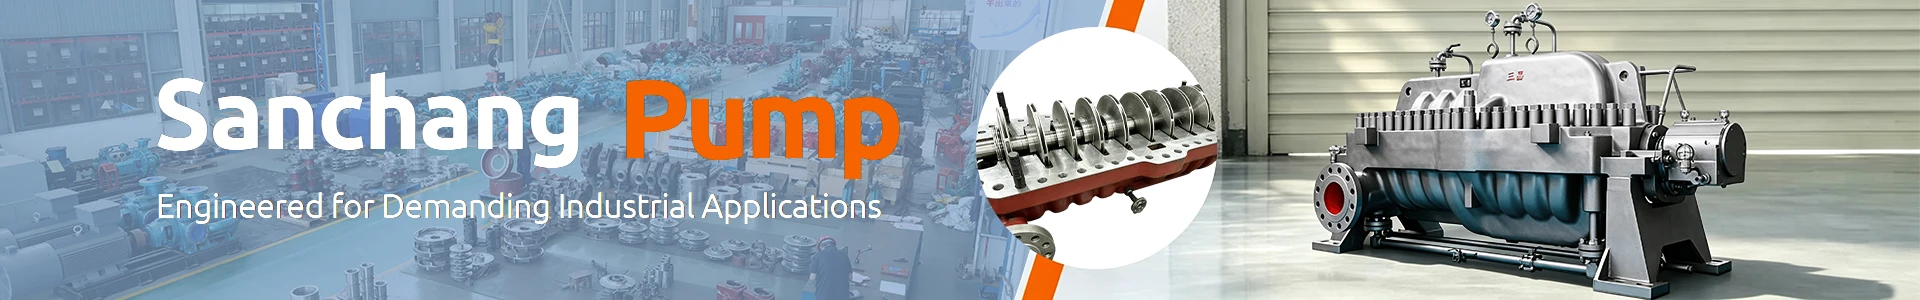
A BB5 double-casing multistage centrifugal pump is widely used for high-pressure services. The outer casing provides pressure containment, while the internal pump cartridge contains the hydraulic components. This configuration can facilitate cartridge removal for maintenance without moving the main casing or disconnecting major process piping.
Wear-Resistant Materials
Coal slurry can contain a high concentration of abrasive solids. Depending on temperature, pressure and slurry properties, pump components may use high-hardness alloys, stainless steels or other wear-resistant materials. Hydraulic passages, impellers and replaceable wear components should be designed according to the actual particle concentration and size.
Mechanical Sealing
Sealing is critical when pumps handle high-temperature, high-pressure, toxic or flammable media. Mechanical seal arrangements should be selected according to operating temperature, pressure, medium properties and applicable API 682 requirements.
Axial Thrust Control
Multistage pumps generate significant axial forces. Back-to-back impeller arrangements, balance devices or other hydraulic thrust-control designs can reduce residual axial load and improve bearing life. Self-balancing multistage designs can also reduce dependence on conventional balance components in suitable applications.
Thermal Management
Coal chemical pumps may operate across a wide temperature range. Thermal expansion can affect casing alignment, clearances and seal performance. Proper warm-up procedures, cooling arrangements and thermal compensation are therefore important for high-temperature services.
3. Standards and Efficiency
API 610 is an important reference for centrifugal pumps used in applicable petroleum and petrochemical services, while API 682 provides requirements for pump shaft-sealing systems.
For low-pressure coal slurry pumps in China's coal-to-liquid chemical industry, NB/T 11685-2024 specifies requirements for centrifugal pumps handling oil-coal slurry or water-coal slurry with solids content up to 70 wt%, viscosity of 700–2000 cP, particle size up to 3 mm and outlet pressure up to 3.0 MPa(G). The standard was issued in September 2024 and implemented on March 24, 2025.
China's GB 19762-2025 establishes minimum allowable energy-efficiency values and energy-efficiency grades for centrifugal pumps and took effect on March 1, 2026.
4. Reliable Pump Solutions for Coal Chemical Applications
Selecting a Coal Chemical Centrifugal Pump requires more than matching flow rate and head. Medium properties, solids concentration, particle size, temperature, pressure, viscosity, corrosion, sealing requirements and installation conditions should all be considered.
For high-pressure and demanding process services, an API610 pump, BB5 double-casing multistage centrifugal pump or customized wear-resistant multistage pump can be selected according to the actual operating conditions.
With application-specific hydraulic design, material selection, sealing solutions and performance testing, centrifugal pumps can provide reliable service across coal gasification, coal liquefaction, methanol production and coal-to-liquid hydrogenation systems.